SST Automation (SSTCOMM) (@sstcomm) header
SST Automation (SSTCOMM) (@sstcomm) profile picture

#industrialautomation company based in California. Experts in HART, ENet/IP, BACnet, Modbus, MQTT/IoT, PROFINet... Inquiries please contact sales@sstcomm.com

California, USA
Joined June 2015
Photo by SST Automation (SSTCOMM) (@sstcomm)Photo by SST Automation (SSTCOMM) (@sstcomm)Photo by SST Automation (SSTCOMM) (@sstcomm)Photo by SST Automation (SSTCOMM) (@sstcomm)Photo by SST Automation (SSTCOMM) (@sstcomm)Photo by SST Automation (SSTCOMM) (@sstcomm)Photo by SST Automation (SSTCOMM) (@sstcomm)Photo by SST Automation (SSTCOMM) (@sstcomm)Photo by SST Automation (SSTCOMM) (@sstcomm)Photo by SST Automation (SSTCOMM) (@sstcomm)
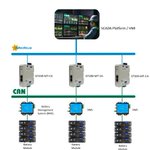
A renewable energy facility had CAN bus-based battery management systems on one network and a Modbus TCP SCADA platform on another. The goal? Get real-time battery data (cell voltages, state of charge, temperatures, fault codes) into the same SCADA interface used to monitor every other asset on site. The catch? They couldn't touch the BMS firmware or redesign the existing SCADA configuration. That would risk too much downtime. So instead of redesigning the system, they deployed SST Automation GT200-MT-CA gateways between the CAN bus BMS units and the SCADA network: → GT200-MT-CA: CAN 2.0A/2.0B to Modbus TCP Each gateway translates CAN frames from the BMS into Modbus TCP registers. CAN ID filtering maps only the relevant battery data to specific registers. From SCADA's perspective, every BMS unit looks like a standard Modbus TCP device. The result: full battery visibility from the existing SCADA interface, commissioning completed in days, zero downtime. And the architecture scales. Every time a new battery module is added, one more GT200-MT-CA gateway connects it to SCADA without any redesign. If your energy storage facility runs CAN bus BMS units and you need them visible in Modbus TCP SCADA, this is how you bridge that gap. #CANBus #ModbusTCP #SCADA #BatteryManagement #EnergyStorage #BESS #ProtocolConversion #RenewableEnergy #IndustrialAutomation #SSTAutomation
1
1
38
A manufacturing facility had DeviceNet drives, Modbus TCP instruments, and HART transmitters all running on separate networks with separate controllers. The goal? Bring everything into one Siemens S7-1500 PROFINET PLC. The catch? Ripping out and replacing field devices wasn't an option. Too expensive. Too much downtime. So instead of replacing hardware, they added three protocol conversion gateways between the field devices and the PLC: → GT100-PN-DM: DeviceNet to PROFINET → GT200-PN-MT: Modbus TCP to PROFINET → GT200-4HT-PN: HART to PROFINET Each gateway translates its protocol into standard PROFINET IO. From the PLC's perspective, every device on the plant floor looks like a native PROFINET device. No custom programming. No special function blocks. The result: full deployment in a couple of days, zero downtime, and unified visibility across all field devices from one HMI (Human-Machine Interface). If your plant floor runs multiple protocols and you're trying to consolidate into one PLC, this is how you do it without a full system redesign. Swipe for the full Case Study. #PROFINET #DeviceNet #ModbusTCP #HART #IndustrialAutomation #ProtocolConversion #Siemens #PLC #SSTAutomation
2
2
76
Most HART gateways give you 1 channel. Maybe 4. The GT200-8HT-EN gives you 8. 8 fully independent HART channels, each supporting up to 15 devices for a total of up to 120 HART instruments through a single gateway into your Modbus TCP network. For process facilities with large HART instrument populations, this gateway eliminates the need to stack multiple single-channel units across your cabinet. One device handles what used to take an entire row of gateways. What sets it apart: → 8 independent HART channels with built-in 250Ω termination resistors → Full HART 5, 6, and 7 support with up to 120 user commands → NE107 device health diagnostics with real-time status mapping and LED alarms → Modbus TCP Server with 8 concurrent connections and 3,000 bytes I/O → Compatible with Rosemount, Endress+Hauser, KROHNE, and Yokogawa instruments → Integrates with any Modbus TCP-compliant PLC, DCS, SCADA, or AMS If you're managing dozens of HART transmitters and tired of a cabinet full of single-channel converters, this is the gateway that consolidates it all. Learn more at sstautomation.com How many HART instruments are you managing at your facility? Tell us in the comments. #HART #ProcessAutomation #ModbusTCP #SSTAutomation #IndustrialAutomation #Instrumentation #SCADA #DCS #ProcessControl #OilAndGas #WaterTreatment #ChemicalPlant
1
37
The equipment works. The inverters work. The batteries work. They just can't talk to each other. Every renewable energy site is a multi-protocol environment. The equipment comes from different manufacturers, built on different communication standards, and none of it was designed to talk to each other natively. That's where SST Automation fits in. Our industrial protocol gateways bridge the communication gaps across solar, battery energy storage, and grid infrastructure so that operators get unified visibility and control without replacing the equipment that's already working. Whether you're integrating Modbus field devices into an IEC 61850 substation, connecting CAN-based battery systems to an EtherNet/IP controller, or pushing site data to a cloud MQTT platform for remote monitoring we've built the gateways that make it work. Learn more at sstautomation.com #RenewableEnergy #SolarPower #BESS #BatteryStorage #SSTAutomation #IndustrialAutomation #IEC61850 #ModbusTCP #CANopen #EtherNetIP #SmartGrid #EnergyStorage #CleanEnergy
2
203
What happens to your Modbus field devices when your PLC fails? In most setups, the answer is simple: you lose visibility. Power meters, flow meters, sensors. All your data goes dark until the PLC is back online. With the newest version of the GT200-PN-RS it now supports PROFINET S2 Redundancy, meaning it can maintain simultaneous connections to two PLCs. If the primary controller fails, the backup takes over instantly. Your Modbus data keeps flowing. No interruption. No manual switchover. No downtime. Why this matters for critical applications: → Water treatment: continuous flow monitoring can't afford gaps → Power generation: loss of metering data triggers compliance issues → Pharmaceutical manufacturing: batch processes require uninterrupted data logging → Any facility where an unplanned data gap means production stops The GT200-PN-RS connects your Modbus RTU and serial devices to PROFINET networks, and now it does it with built-in redundancy that matches the reliability your process demands. Learn more at bit.ly/4g1p7j8 Has a PLC failure ever caused a data gap on your plant floor? How long did it take to recover? #PROFINET #ModbusRTU #IndustrialAutomation #PLCRedundancy #SCADA #ProcessAutomation #SystemIntegration #WaterTreatment #SmartManufacturing #Siemens #ProtocolConversion
2
540
Every facility wants predictive maintenance, remote monitoring, and cloud dashboards. But most Siemens PLCs that are currently in-use were built before any of that existed. They have an MPI or PPI port and no way to connect to modern Ethernet-based platforms. A lot of companies assume that means a full PLC replacement, new hardware, rewiring, reprogramming, downtime. That's a big project with a big budget. The GT100-IE-MPI makes the first step toward modernization the easiest one. Plug it into the PLC's PPI/MPI or PROFIBUS port, connect an Ethernet cable, and configure it from a web browser. No rack modifications, no external power supply, and no additional software to install. Your existing PLC is on Ethernet and accessible to STEP 7, TIA Portal, WinCC, KEPServerEX, Ignition, or any S7 TCP/IP compatible platform in minutes, not weeks. → Compatible with S7-200, S7-300, S7-400, and CNC 840D/840DSL → Supports PPI, MPI, and PROFIBUS in one adapter → 16 simultaneous Ethernet connections → Built-in Modbus TCP server for additional monitoring connectivity → Web-based configuration from any device with a browser You don't need to replace a PLC that still works. You just need to give it an Ethernet port. Learn more at sstautomation.com What would you connect to your PLC first: SCADA, remote access, or cloud monitoring? Tell us in the comments. #Siemens #S7300 #S7400 #PLC #SSTAutomation #IndustrialAutomation #DigitalTransformation #SCADA #PredictiveMaintenance #SmartManufacturing #Retrofit
2
88
Buildings produce 40% of global carbon emissions. A new ASHRAE study just confirmed that BACnet-based building automation has already prevented 1.4 BILLION tons of CO2 emissions and could hit 2.06 billion tons by 2030. But here's the problem nobody's talking about: Millions of buildings have BACnet controllers and Modbus devices already installed, but they're confined to local networks. No cloud visibility. No AI optimization. No remote monitoring. The data is right there, just waiting to be connected to the cloud. That's exactly why we built the GT200-MQ-BMT. It takes your existing BACnet controllers (like Johnson Controls) and Modbus TCP devices and bridges them directly to MQTT cloud platforms like Microsoft Azure, Amazon Web Services (AWS), or your own custom server. No ripping out equipment. No six-figure integration projects. No downtime. Plug it in → your building data flows to the cloud → unlock AI-driven energy optimization, predictive maintenance, and real-time remote monitoring from anywhere. → One gateway. Two protocols. Unlimited cloud potential. What would you do with real-time building data in the cloud? Comment your use case below. Learn more: sstautomation.com #SmartBuildings #BuildingAutomation #BACnet #Modbus #IoT #Decarbonization #EnergyEfficiency #HVAC #FacilityManagement #IIoT #SSTAutomation #AI #ArtificialIntelligence
1
2
2
616
According to @Siemens , unplanned downtime costs manufacturers an average of $260,000 per hour. Network failures account for 16% of it. That's production time you're not getting back. Most EtherNet/IP networks still run linear or star topologies. When a cable fails or a device drops, everything downstream also fails. The PLC loses visibility. The line stops. And the clock starts. Device Level Ring Redundancy (DLR) changes the math. A ring topology with sub-3ms recovery means a cable fault doesn't become a production outage, the network reroutes before the next scan cycle completes. SST Automation now offers a complete EtherNet/IP DLR solution: → GT300-EI-2RS485: Modbus-to-EtherNet/IP gateway with native DLR support → ETAP-G5-DLR: 5-port Gigabit DLR that acts as ring supervisor or node, connects non-DLR devices to active rings" If you're already running EtherNet/IP and haven't looked at DLR, the question isn't whether you need network redundancy. It's how many hours of downtime are you're willing to risk before you add it. Learn more → sstautomation.com #EtherNetIP #DLR #IndustrialAutomation #NetworkRedundancy #ManufacturingDowntime #SSTAutomation
1
65
The hardest part of connecting a renewable energy site to the grid isn't permitting, financing, or construction. It's getting the equipment to talk to each other. The renewable site speaks Modbus. The utility substation speaks IEC 61850. Inverters, power meters, weather stations, PLCs nearly all of them communicate via Modbus RTU or TCP. But the moment that energy connects to the grid, the automation system on the other side expects IEC 61850. This protocol mismatch is slowing down interconnections at a time when the renewable energy queue has never been longer. The GT850-ES handles both sides: → Modbus RTU via dual RS-485 (serial field devices) → Modbus TCP via dual Ethernet (networked devices) → Translates everything into a single IEC 61850 data model for the utility No rip-and-replace. No extra conversion layers. One gateway at the point of interconnection. If you're integrating renewable generation into utility-grade substation networks, the GT850-ES was built for this exact handoff. Have you hit this protocol mismatch on a project? How did you solve it? #RenewableEnergy #IEC61850 #Modbus #SubstationAutomation #SmartGrid
1
31
Centralized refrigeration monitoring is no longer a nice-to-have. With tightening EPA regulations and increasing pressure to track, document, and optimize cooling system performance, facilities need real-time visibility into every refrigeration unit on the floor, not just the ones near the control room. But here's the challenge most plants run into: The refrigeration units communicate through a CANopen-based controller. The field instruments and PLCs at each workstation communicate over Modbus RTU. Two different networks. No shared language. That's the gap the GT200-CO-RS closes. Recently, the GT200-CO-RS was deployed as the communication bridge between Modbus RTU field devices and a CANopen central controller at a few sites with industrial cooling installed. The gateway collects temperature, pressure, and flow rate data from refrigeration units across multiple workstations and translates the data for the central control system in real time. The result: → Real-time operating data from every refrigeration unit in one place → Bidirectional Modbus RTU to CANopen protocol conversion → Centralized monitoring, fault diagnosis, and control logic management → Industrial-grade EMI immunity for harsh equipment room environments When your cooling systems are optimized, your product quality stays consistent and your equipment lasts longer. Centralized visibility is how you get there. Learn more at sstautomation.com What cooling or refrigeration challenges are you dealing with? Tell us in the comments. #IndustrialRefrigeration #CAN #ModbusRTU #ProtocolGateway #SSTAutomation #ProcessControl #SCADA #IndustrialAutomation #RefrigerationMonitoring #FoodSafety #ManufacturingExcellence #TemperatureControl #ArtificialIntelligence #AI
1
3
69
Water utilities are modernizing their SCADA systems faster than ever. Yet, most field devices like flow meters, level sensors, pressure transmitters, VFDs still communicate over Modbus RTU / RS485. Modern monitoring platforms run on Ethernet. The field devices don't. The GT200-MT-RS485 bridges that gap connecting your existing Modbus RTU/ASCII serial instruments to a Modbus TCP Ethernet network. Bidirectional. Up to 16 TCP/IP connections. No device replacements needed. SCADA modernization doesn't have to mean replacing all your field devices. Often the smartest upgrade connects what you already have. sstautomation.com #WaterAndWastewater #SCADA #ModbusTCP #ModbusRTU #SSTAutomation #IndustrialAutomation #SmartWater #ArtificialIntelligence #AI
1
2
46
Everyone's talking about AI on the factory floor in 2026. Predictive maintenance. Cloud dashboards. Real-time analytics. But here's what most people are overlooking: Most plants still don't have a direct path from their field devices to a cloud platform. The Modbus RTU sensors, meters, and instruments that run your operation weren't built to talk to AWS, Azure, or any MQTT broker. They were built to talk to a PLC sitting 10 feet away. That's not an AI problem. That's a protocol problem. The GT200-MQ-IE is a Modbus and EtherNet/IP to Cellular MQTT gateway that bridges that gap. It collects data from your existing Modbus RTU/ASCII, Modbus TCP, and EtherNet/IP master devices and publishes it directly to your cloud platform over 4G/5G no middleware, no PC in the middle, no IT project. → Connects Modbus serial, Modbus TCP, and EtherNet/IP master devices to any MQTT broker → 4G/5G cellular with built-in GPS for remote or distributed sites → 2 digital inputs + 2 digital outputs for local monitoring and control → Secured with SSL v3.0 and TLS v1.2 encryption → JSON format, compatible with any IoT platform You don't need to replace your field devices to go digital. You just need to give them a way to talk to the cloud. Learn more at sstautomation.com What legacy protocol is holding up your IoT project? Tell us in the comments. #Industry40 #IoT #MQTT #ModbusToCloud #SSTAutomation #PredictiveMaintenance #DigitalTransformation #SmartManufacturing #IndustrialAutomation #SCADA #OTtoIT #EdgeComputing #PLC #ArtificialIntelligence #AI
1
56
Improving data center power infrastructure should be about expanding capacity and reliability, not protocol mismatches. CANopen batteries. EtherNet/IP control system. The GT200-EI-CO bridges them! Translating battery data into native EtherNet/IP so Uninterruptible Power Supply (UPS) systems appear as standard Ethernet-connected assets. Case study from previous data center project→ sstautomation.com/Use_Case/G… #DataCenter #CANopen #EtherNetIP #ProtocolGateway #SSTAutomation
1
27
The data center industry has a problem money can't solve. → Vacancy: Under 1% → Grid connection wait: 4+ years → 92% of capacity under construction: already pre-committed The fastest path to new capacity? A building that already has power. Companies in need of data centers are looking to convert factories, warehouses, and offices into data centers at record pace. However, the existing infrastructure (HVAC, generators, power systems) speaks Modbus, while Modern platforms expect BACnet, and MQTT for cloud connectivity. SST protocol converters bridge that gap, no system redesign needed. Deployed across active DC projects with leading general contractors, integrators, and operators. sstautomation.com #datacenter #adaptivereuse #protocolgateway #BACnet #Modbus #MQTT #buildingautomation
1
35
Integrating Modbus RTU/TCP devices into an IEC 61850 network? GT850-ES bridges both Modbus RTU and TCP into IEC 61850; dual RS-485, dual Ethernet, one box. In stock. Direct engineering support from SST. #IEC61850 #ModbusTCP #SubstationAutomation #SCADA
1
104
Modernizing a factory floor often leads to a compatibility gap between high speed EtherCAT networks and essential serial field devices. When you are running a system with OMRON or Beckhoff PLCs, it is frustrating to find that your existing sensors or drives cannot communicate with the newer architecture without a significant workaround. The GT200-EC-RS is designed to bridge this gap by bringing Modbus RTU or ASCII devices directly into the EtherCAT environment. As illustrated in the application diagram, it allows for a unified connection between your controllers and a wide range of RS-485 hardware such as weighing instruments, VFDs, and laser rangefinders. With a high data capacity of 512 bytes for both Input and Output, it can handle data intensive applications without becoming a bottleneck in your data stream. Instead of writing complex drivers or replacing perfectly good hardware, you can use our configuration software to map registers quickly. This software includes diagnostic tools that help you verify data flow during the setup phase, which significantly reduces the time spent on commissioning. The gateway is built for industrial reliability, ensuring that your communication remains stable even in demanding factory settings where uptime is critical. Using the GT200-EC-RS allows you to maintain your current investment in field assets while taking full advantage of the speed and precision that EtherCAT offers. It is a straightforward way to achieve better data visibility and a more connected manufacturing process. Learn more at our website: sstautomation.com/Products/E… Technical Support: support@sstautomation.com Sales Inquiry: sales@sstautomation.com #IndustrialAutomation #EtherCAT #Modbus #SSTAutomation #Manufacturing #Engineering #PLC #IIoT #SmartFactory #RS485
1
83
Many industrial environments still rely on HART-enabled field devices for critical process data, but integrating these devices into modern PROFINET-based control systems is often complex and inefficient. Engineers frequently encounter challenges with multi-device communication, limited diagnostics, and lengthy commissioning times, especially when scaling systems or maintaining legacy infrastructure. The GT200-4HT-PN gateway provides a streamlined way to connect HART devices directly to PROFINET networks. Designed with flexibility in mind, it supports up to four HART channels and can operate as either a primary or secondary master, enabling smooth integration without disrupting existing setups. At its core, the gateway enables four-channel HART polling communication, supporting both point-to-point and multi-drop modes while remaining compatible with HART 7 and earlier protocols. On the PROFINET side, it operates as a slave device and supports RT and IRT communication for real-time data exchange. With configurable input and output data sizes of up to 1440 bytes, engineers can tailor data handling to their specific PLC environment. The included SST-HPN-CFG configuration software enhances usability by providing clear data visualization, command diagnostics, and efficient debugging capabilities, significantly reducing setup time. The result is faster system commissioning, improved access to device-level diagnostics, and a significant reduction in integration complexity. By enabling reliable, high-speed communication between legacy HART devices and modern PROFINET systems, the GT200-4HT-PN helps organizations extend the life of existing assets while advancing toward smarter, more connected industrial operations. Learn more: sstautomation.com/Products/H… For Technical Support: support@sstautomation.com For Sales Inquiry: sales@sstautomation.com #IndustrialAutomation #PROFINET #HART #IIoT #SmartManufacturing
1
54
Bridge Modbus RTU and BACnet/IP networks with the GT200-BM-2RS. This robust gateway supports hundreds of BACnet objects and features dual RS485 ports for maximum scalability. Contact our team today for integration support. #BACnet #Modbus #Automation #SCADA #SmartBuildings
1
1
2
117
How do we move from 'Existing+' to 'Orchestrator'? 🚀 MIT Sloan's new framework highlights the shift towards AI-mediated collaboration. At SST Automation, our MQTT Gateways provide the real-time, bi-directional data flow that makes this transition possible. Whether you are integrating with #Kepware environments or building next-gen #AIoT solutions, the key is turning raw device data into actionable AI insights. 🌐🤖 #MITSloan #IndustrialAutomation #MQTT #DigitalTransformation
With the rapid adoption of AI technologies, @MIT_CISR created a business model framework for the AI era that shows businesses evolving to become increasingly outcome oriented and enabled by autonomous AI. Learn more: bit.ly/4qWCWlH
2
59
SST Automation (SSTCOMM) retweeted
Beyond the Cable Run: Industrial PoE Solutions Built for the Remote Edge industrialethernet.net/techn… Power over Ethernet (PoE) reliably delivers power to remote sites with a single Ethernet cable delivering both power and data over long distances acts as the enabling technology. #PoE #poweroverethernet #antaira
1
1
108